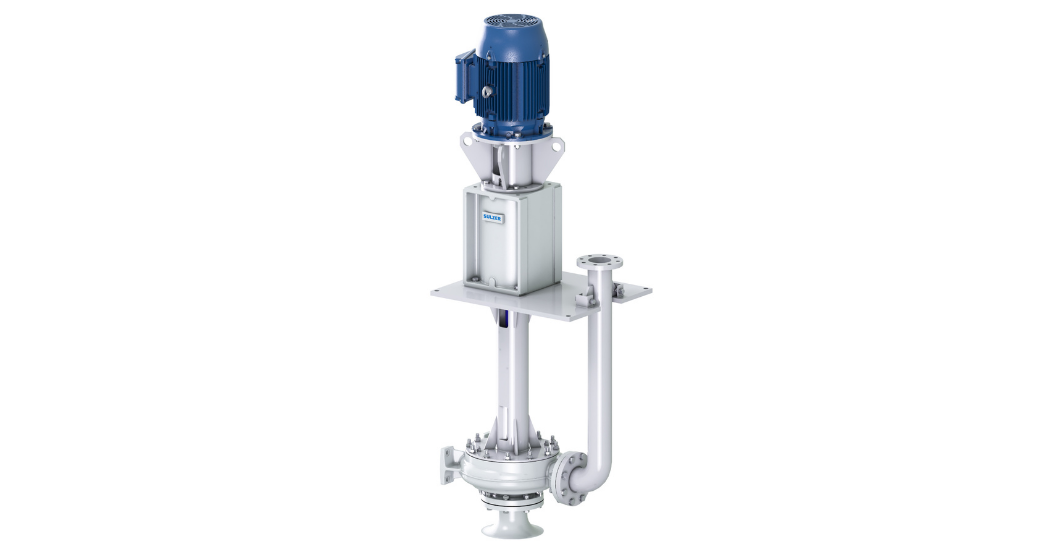
Sulzer launches an upgrade of the VA vertical cantilever sump pump. The VA pump range has been designed for pumping all kinds of clean and contaminated liquids and slurry. Thanks to its great adaptability through a wide range of designs and hydraulics, the VA pump is perfectly suited to all industrial applications.
The main purpose of the upgrade project was to develop a rigid and reliable cantilever sump pump that contains Sulzer’s most efficient hydraulics. The hydraulic coverage was extended with energy-efficient, non-clogging and wear-resistant options, and it now includes the core process and slurry pump portfolio hydraulics. With the upgrade, multiple improvements were also made to the vertical construction.
The VA pump is suitable for highly demanding applications such as:
- Industrial water
- Effluents
- Corrosive and abrasive mixtures
- Hazardous fluids
- Abrasive liquids and/or liquids containing large solids
- Abrasive fibrous slurries and/or fibrous slurries containing large solids
- Abrasive non-fibrous slurries and/or non-fibrous slurries containing large solids
- Heavy slurry
Sulzer’s VA pumps come with high reliability and performance. An extensive range of materials, including abrasion-resistant and corrosion-resistant options, ensures exceptional resistance against wear and guarantees high durability of the pump.
Learn more about the technical details of the upgraded VA cantilever sump pump range on their website.
Follow Sulzer Industry on LinkedIn.
About Sulzer
Sulzer is a global leader in fluid engineering. We specialize in pumping, agitation, mixing, separation and application technologies for fluids of all types. Our customers benefit from our commitment to innovation, performance and quality and from our responsive network of 180 world-class production facilities and service centers across the globe. Sulzer has been headquartered in Winterthur, Switzerland, since 1834. In 2020, our 15’000 employees delivered revenues of CHF 3.3 billion. Our shares are traded on the SIX Swiss Exchange (SIX: SUN).
The Flow Equipment division specializes in pumping solutions specifically engineered for the processes of our customers. We provide pumps, agitators, compressors, grinders and screens developed through intensive research and development in fluid dynamics and advanced materials. We are a market leader in pumping solutions for water, oil and gas, power, chemicals and most industrial segments.