Overview
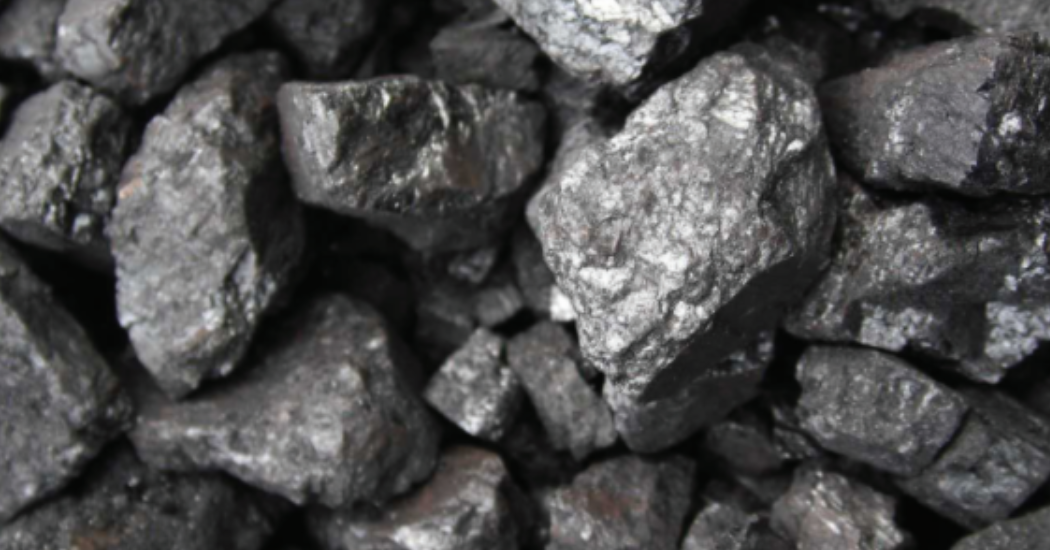
PABTEX, L.P., located in Port Arthur, Texas, is a bulk commodity handing facility and vessel loading terminal that exports petroleum coke (petcoke). PABTEX stores up to 500,000 tons of petcoke before transferring to shipping terminals for transport to customers globally.
Raw petcoke is transported to the terminal in bottom dump railcars, then processed through shakers to break it into smaller chunks for easier conveyor transport. Beneath the shakers is an 80ft deep conveyer shaft. Rainwater routinely fills up this conveyer shaft, and requires a large sump pump to reroute rainwater to a retention pond. With the shakers directly above the conveyor shaft, pieces of abrasive petroleum coke fall into the shaft, and routinely clogging the pumps.
After trying several submersible pumps for the conveyer shaft sump application, the maintenance supervisor for Savage Gulf Services which operates the PABTEX Port Arthur terminal, sought out their pump supplier for a new pump solution.
“Pumping reliability is critical to the overall refining process,” PABTEX and Savage Gulf Services
Solution
Together with his pump distributor, the maintenance supervisor selected the Industrial Flow Solutions™ BJM Pumps® KZN series abrasion-resistant, solids-handling pump. KZN pumps feature wet end parts made of abrasive-resistant chrome iron for maximum wear. The 28% high chrome agitator is specifically designed for sand, sludge and slurry applications. It keeps solids from settling in the slurry, which makes it easier to pump with less chance of clogging. A semi-open impeller and wear plate handles solids concentrations, as high as 70% by weight, of the abrasive petcoke.
KZN series pumps feature double silicon carbide mechanical seals that separate the oil-filled seal chamber and a heavy-duty lip seal for additional mechanical seal protection. These top-discharge pumps are cooled by the pumped liquid, and do not need to be fully submerged. Instead, they can pump down to just a few inches of slurry and still maintain operable motor temperatures. (The other pumps left 3ft of un-pumped slurry because they had to be submerged to avoid overheating).
The KZN series pump was installed for a 60-day trial and was purchased after zero clog and wear issues.
The KZN was so successful, a second was purchased 2 months later.